

FAQs
How Critical Are Mix Ratios?
Catalytic-cure polymers, like polyesters, will cure with any amount of catalyst added. A catalyst just starts the reaction. The more catalyst, the shorter the pot life and faster the cure time. Epoxies and urethanes, with a few exceptions, are designed to cure at an exact mix ratio, which allows each molecule of resin will crosslink with a molecule of hardener. Off-ratio mixes result in excess resin or hardener molecules that have nowhere to attach, which results in deteriorated properties.
Each resin/hardener mixture has a tolerance for error. Generally speaking, for epoxies it is safe to use ratios within 10% of the exact ratio and within 5% for urethanes. Beyond these tolerances, the systems may still cure, but with degraded properties. This is especially true for high-temperature systems where the first property affected from being off ratio is the Heat Distortion Point (HDT). If the system is far enough off ratio, it will only partially cure and be obviously unusable.
It is important to note that the target mix ratio should be the one that is published. The tolerance range allows for slight errors in measurement. To intentionally measure off ratio is never advised. Some epoxy hardeners are formulated to be “variable-ratio hardeners”. The published ratios for these hardeners will show a range of acceptable mix ratios.
Be aware of smaller batch sizes where more accuracy is required to be on ratio. Likewise, low-ratio systems like 100:5 or 100:10 need to be weighed more accurately then high-ratio systems like 100:50.
What Is The Best Method For Measuring Mix Ratios?
Mix ratios are stated in two ways, by weight and by volume. Weighing is the most accurate method of measuring ratios. Weight ratios are designated as parts-by-weight (pbw) or parts-per-hundred (pph). The weight ratio will be shown as 100:15 pbw, for example. This means every hundred parts of resin needs 15 parts of hardener for complete reaction. Example: A 300-gram batch of resin at 100:15 pbw mix ratio needs 45-grams of hardener.
Volumetric ratios are primarily used for dispensing equipment. These ratios are expressed in two ways: parts-by-volume (pbv) or by a ratio. A volumetric ratio could be stated as 100:25 pbv or 4:1 by volume.
Some, who do not have a scale for weight measurement, use graduated containers to measure by volume. This works where the ratios are even, like 1:1, 2:1, 4:1, etc. Volumetric measuring becomes a problem when the ratios are uneven, such as 100:17.35 pbv, or 5.75:1 by volume. Chances of being off ratio are increased by measuring volumetric ratios by hand.
Can Pot Life Be Adjusted By Changing The Mix Ratio?
Epoxies and urethanes are designed with one exact mix ratio. It is not recommended to lower the mix ratio during hot weather to increase the pot life. Likewise, ratios should not be increased during cold weather to speed up resin systems.
During hot weather it is best to mix smaller batch-sizes at the correct ratio, or use a slower-reacting hardener at its correct ratio. During cold weather, larger batches can be mixed, or a faster-setting hardener used to speed reaction time. Changing mix ratios to adjust pot life is always dangerous.
What Factors Effect Pot Life And Cure Time?
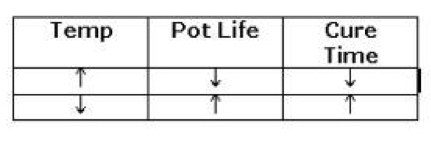
Factors that directly influence pot life and cure times are: Working temperature, mass of the mixed material, and the speed of the hardener. Pot life is measured in the lab at an ambient temperature of 25° C. (77° F.). There is a general rule-of-thumb for epoxies that for every 10° C. the temperature goes up, the pot life and cure time will be reduced by half. If it increases by 20° C., the times will be cut in half, and cut in half again. This rule is also generally true in reverse; for each 10° C. decrease in temperature, the pot life and cure time will double.
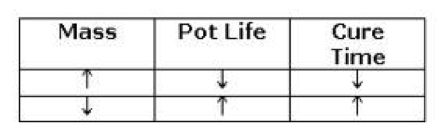
Pot life is measured in the lab for a certain mass of mixed material, usually 100-grams unless otherwise stated. As the mass of the mixed material increases, the pot life and cure time decrease. As the mass decreases, the pot life and cure time increase.
The choice of hardener affects the pot life and cure time of a system. One epoxy resin can be used with a large number of different speed hardeners to get a wide range of pot life and cure times. Please call us if a special resin/hardener combination is required for specific pot life and cure time requirements.
What Is An Exothermic Reaction?
Epoxies and urethanes (to a lesser extent) create heat when the resin and hardener crosslink, or chemically combine. This internally generated heat is called exotherm, and is a necessary by-product of the curing cycle. When exotherm becomes excessive it results in the resin boiling, smoking, shrinking and emitting strong odors. Choosing correct hardener speed, controlling ambient temperatures, and limiting the mass of the mixed material are ways of minimizing exothermic reactions. If large mixes are required for a job, use a slower reacting hardener. If a specific hardener has to be used, mix smaller batch sizes. A mass of material will exotherm more quickly when left in a concentrated volume, than if it was spread over a larger area. When mixing large amounts of material, pot life can be extended by pouring off into smaller containers and working out of those.
If a mixing cup starts to exotherm, place the container either outside or in a well-ventilated area. Submerging in water will stop the exothermic reaction. Never place a container that is exotherming into a trashcan that contains combustible materials.
What Is The Difference In The Terms: Pot Life, Gel Time, Working Time, Tack-Off Time, Etc.?
Pot Life and Gel Time are used interchangeably – This measurement is made in the lab under controlled conditions, usually at 77° F. and in a 100-gram mass. This is usually tested in an XXX Gel Timer instrument, which rotates a wire hook in the liquid mixture until it thickens to the point where it reaches a predetermined torque level and shuts off. The machine then records the elapsed time. Working Time – The time it takes for a mixture to reach a viscosity where it becomes unworkable. For example: the point where a laminating resin becomes too thick to wet-out fabric. The material may have not gelled at this point; it is just too thick to do the job for which it was intended.
Tack Time – The time for a mixture to cure to the point where it is “rubbery”. At this point you can leave a fingerprint on the surface of the system and it will not transfer to your finger. This is the ideal time to bond one layer of liquid epoxy or urethane to a cured layer, i.e., to laminate against a surface coat.
Tack-Off Time – The time for a system to become hard to the touch, with no tackiness. This is a good time to sand the surface, without gumming up the sandpaper. If an epoxy surface has reached this level, it must be sanded before another layer of liquid epoxy is bonded to it. At this point, the resin system is only partially cured. Demold Time – The time for a resin system to cure to the point where it can be removed from the mold without distortion. It is not fully cured at this time.
Cure Time – The time it takes a system to reach full properties. This time can be measured after a room-temperature or an elevated-temperature cure.
Do Epoxies And Urethanes Outgas?
The epoxies and urethanes we formulate do not contain solvents. Our systems are “100% solids”, which means all the ingredients, when combined at the proper mix ratio, react completely with no outgassing. Once cured, the chemicals are linked together and not able to come off as a vapor.
Why Do High-Temperature Epoxies Change Color After Exposure To Elevated Temperatures?
Most high-temperature epoxy systems will darken due to amine-based hardeners, which darken with heat. Do not confuse this darkening with a deterioration of properties. It is possible to char an epoxy laminate or casting if it is heated far above its maximum temperature. Some hardeners cause epoxies to have a dark-reddish cast after heat exposure. This is a normal reaction of certain hardeners. The epoxy has not been burnt.
What Is The Difference Between Glass Transition Temperature And Heat Deflection Temperature?
Both processes measure the same thing, the point where the cured resin goes through a change in its molecular structure. At this point mechanical properties decrease at an increasing rate and the coefficient of thermal expansion increases.
Heat Deflection Temperature (HDT) is a mechanical method of measuring this point. A cast bar measuring ½” X ½” X 5” is suspended between two points 4” apart. A load is applied halfway between the two suspension points. The entire apparatus is submerged in an oil bath, with the temperature of the oil raised at a set rate. When the cast bar deflects 0.010-inches under the load, the oil temperature is recorded as the HDT. This number is commonly reported at two load levels, 64 psi and 264 psi. Measuring HDT is a time consuming procedure that can tie up a lab technician for hours.
Note: Some companies report high HDT numbers by testing laminates instead of cast bars. Fiber reinforcement keeps the bar from deflecting even after the resin system has passed its HDT. These numbers do not accurately represent the capacity of a resin system. Glass Transition Temperature (Tg) is a computerized method of measuring the molecular change. There are three types of equipment used to determine Tg, by different measuring methods: Differential Scanning Calorimeter (DSC), Dynamic Mechanical Analyzer (DMA) and Thermal Mechanical Analyzer (TMA). The chemist decides which equipment is the most accurate for a particular product. Any of these methods are much faster than measuring HDT.
Epoxy HDT and Tg measurements are highly correlated. Flexible urethane elastomers exhibit no meaningful HDT or Tg numbers. Rigid urethanes are measured by both methods, with HDT giving more consistent and relevant results.
Can A Tool Be Used Above Its Glass Transition Or Heat Deflection Temperature?
An epoxy tool will not fall apart, or be unusable, because it was heated above the HDT or Tg point. Fiber-reinforced laminates can operate at higher temperatures. Just be aware that the HDT or Tg point is where mechanical properties start to drop at an increasing rate. Most tools are over designed and are much stronger than need be. It is like a yellow caution light warning of trouble ahead. The Tg point is important for tight-tolerance tools since the coefficient of thermal expansion increases at that temperature. Molding parts at temperatures over the tool’s Tg can cause dimensional problems.
How Important Is Post-Curing For High-Temperature Tooling?
Many of our high-temperature systems are what we call “Room-Temp-Set, Hi-Temp Systems”. This means the resin will cure enough at room temperature for the tool to be removed from the pattern and be given an unsupported post-cure. At this point the material does not have its high-temperature properties.
These types of resin systems have components that cure hard at low temperatures, to give enough strength for demolding. Other components do not crosslink until they see higher temperatures. The first time the resin sees increased temperatures, it softens as crosslinking occurs. It is best to let this reaction happen under controlled temperature increases, without loading the tool. Once the tool has been properly post-cured, it can be exposed to higher temperatures without softening.
Can Epoxies Be Bonded To Cured Epoxy?
Epoxies do not bond well to each other if one surface has cured to a hard glazed-over condition. The glazed surface must be roughed up by sanding, before applying fresh resin. If left unsanded, the bond will be tenuous and likely to separate or chip off at some later time. An example of this is laminating behind a glazed surface coat. If the back of the surface coat is not sanded, it will separate from the laminate when either being exposed to high temperatures or being flexed during service.
How Can Empty Containers Be Disposed?
Click to download the PDF version of Report From Department of Toxic Substances Control
How do you properly mix surface coats?
Proper mixing of surface coats is critical because soft spots or uncured material in a tool face can require rework or scrapping of the tool. Refer to FAQ “General Information” for proper weighing methods.
When mixing surface coats, always “double-cup”. This simply means to weigh the resin and hardener into one container and thoroughly mix by scraping the sides and bottom of the container. Transfer the mixed material into a second container and remix in the same manner. This procedure eliminates the possibility of applying unmixed material.
Never mix in only one container, as there is a good chance that either the resin or hardener will cling to the sides, bottom or corners of the container and not be properly blended. Also, never scrape the sides of the container when transferring the material to the working surface.
What is the correct thickness?
For low-temperature applications, surface coat thickness is not critical. It should be applied just thick enough to get the job done. If the tool surface needs to be high-wear, or requires sanding to control finish or contour, then apply a thicker coating. Thicknesses greater than 0.080-inches are not usually recommended.
High-temperature surface coats should always be kept as thin as possible. The reason is there are large differentials in coefficients of thermal expansion (CTE) between surface coats and laminates. As the tool heats and cools a surface coat will expand and contract at a much greater rate than a laminate. A thick surface coat will build up more stress than a thin coat, which results in cracking.
Ideally, a high-temperature surface coat will have cloth worked into the back surface. This is not usually practical because any scribing or sanding will expose the cloth and compromise vacuum integrity. Thicknesses in the 0.015-0.030 inch range work well for high-temperature applications.
Be aware of allowing surface coats to drain off of vertical surfaces and mass on inside corners of the pattern. These areas can build up quite thick, which become the external corners of the tools. These are the areas that are most prone to cracking and chipping.
How should surface coats be applied?
Epoxy surface coats are best applied by brushing or spreading with a rubber squeegee. For paste surface coats, use a short-bristle brush, like the PTM&W Tooling Brush, or cut the bristles of a normal brush to ¾ – 1 inch long. For softer, lower-viscosity surface coats, regular length bristles are adequate. Brushing is the best method when the pattern has a lot of contour or detail.
Spreading surface coat with a squeegee is the preferred method when large, low contour, smooth surfaces are to be covered. Use a paint thickness gauge to control application thickness.
Can epoxy surface coats be sprayed?
Unlike polyester gel coats, epoxy surface coats are generally not sprayed. Epoxies are usually thicker and have higher surface tension, which makes spraying difficult. When spraying is attempted, epoxies tend to “fish-eye” and not leave a smooth solid surface.
Some of the lower-viscosity epoxy surface coats have been successfully sprayed by using a stucco gun, which splatters the material on the pattern surface. This is just a method of getting the surface coat evenly distributed on the pattern surface. The sprayed material then has to be brushed smooth.
Do not use solvents to thin epoxy surface coats to make them more sprayable.
Should surface coats be applied in one or two coats?
Both methods are acceptable. The advantage of one coat is it is easier to keep the surface coat thin. The drawback is that it is easy to push cloth through the surface coat if applied too soon. With two surface coats, the first coat can be allowed to gel to the point where cloth will not push through.
Always allow the first coat to gel to the “finger-print-stage” where you can leave a finger print on the back surface and it will not come off on your finger. This is the proper time to start laminating or apply the second surface coat.
One method used for high-temperature surface coats is to work the first ply of laminate into the second surface coat while it is wet. If the laminate is going to be vacuum-bagged, the second surface coat can be mixed with the same long pot-life hardener as the laminating resin allowing the second coat to stay liquid while being bagged. This allows the first layer of cloth to be pressed into the surface coat.
If this process is used, some toolmakers will mix the second surface coat and the laminating resin with the same long pot-life hardener. The two are then blended at a ratio (usually 50:50) to get the desired consistency. This method changes the viscosity of the second coat to somewhere between the surface coat and the laminating resin, which helps in wetting-out the first layer of cloth.
What causes soft spots in surface coats?
Soft spots in cured epoxy surface coats are always caused by improper mixing. Use the “double-cup” method.
What causes “fish-eyes”?
“Fish-eyes” are areas in a freshly applied surface coat that tends to thin or open up on their own accord. Sometimes, these spots can be re-brushed and still continue to open. This problem is caused by the high surface tension of the epoxy applied on a slippery surface, such as a silicone-based mold release. Some surface coats, usually high-temperature, have more of a tendency to fish-eye than others do.
The best solution is to use a less-slippery mold release, such as a high-temperature paste wax.
Why are surface coats sometimes rubbery?
If the entire surface coat is rubbery, it is do to either not being fully cured or an improper mix ratio. If not cured, the solution is to use a faster setting hardener, or allow more time to cure, or apply heat to increase the cure rate.
Mixing a surface coat off-ratio, with either too much or too little hardener, will cause the material to stay rubbery and not fully cure. If the surface coat is cured hard in some areas and rubbery in others, improper mixing procedures were used.
How do you get rid of porosity in surface coats?
Porosity in surface coats is caused by air induced during the mixing process and/or the application process being trapped when the system cures. One or more of the following may minimize porosity:
- Mix in less air by gently stirring the resin and hardener together instead of vigorously mixing.
- Vacuum de-gassing the surface coat before application.
- Brushing a thin coat to allow air to escape.
- Gently applying heat from a hot-air gun on the back surface of the material. This lowers the viscosity of the system and causes the air bubbles to increase in volume and rise to the surface and pop.
- Using a lower viscosity (thinner) surface coat
What causes blisters in high-temperature surface coats?
Blisters are caused by air trapped in the surface coat (porosity) or behind it. When heated, this air will expand and take the path of least resistance, usually blistering out the face of the tool.
The solution is to minimize porosity (see above question) and eliminate air trapped between the surface coat and laminate. Poor laminating technique causes trapped air. This problem can be minimized by:
- Spending more time and extra care while laminating the first few plies behind the surface coat.
- Applying dry cloth to wet resin, which allows the air to pass through the cloth, instead of wet resin to dry cloth, which forces air to pass through both the resin and the cloth.
- Using a stiff brush to stipple the resin and completely wet-out the cloth.
- Using a ribbed-roller to wet-out the cloth in flat areas.
- Vacuum-bagging the laminate to remove air and excess resin.
What causes cracking in high-temperature surface coats?
Surface coat cracking is caused by it being applied too thick. See above FAQ “What is the correct thickness?”
What causes surface coats to separate from the laminate?
If an epoxy surface coat is allowed to cure to a hard, glassy stage before laminating, it will not properly bond to the laminate. Always start laminating behind a surface coat when the material has reached the “finger-print” stage. If it has cured hard, the back of the surface coat must by sanded to remove the glazed surface.
Why do external corners of a tool easily chip?
Surface coats tend to be hard, brittle non-reinforced materials. They get their strength from the laminate backing them up. If they are thin, they tend to be tough, if thick they tend to chip easily. External corners of tools are made from the internal corners of the pattern. If not carefully applied, surface coats will slide down vertical surfaces and build up in the bottom corners, which causes the cured surface coat to be too thick.
Also, it is sometimes difficult to get the cloth to lie down tight on inside corners. It is easy for the cloth to bridge the corner and create a poor bond between the surface coat and laminate. This makes it easy for the surface coat to chip or break away from the laminate.
Why does a surface coat change color when exposed to high temperatures?
High-temperature hardeners are made up of various components including amines. Certain varieties of this chemical will darken or turn a reddish color when exposed to heat. This change in color does not indicate a problem; it is just a natural occurrence.
What causes “print-through” and “mark-off”?
Print-through is the cloth pattern from the backup laminate showing through the surface coat. Usually this is a cosmetic problem and has no effect on tool performance. It is caused by resin shrinkage in the laminate. When measured in the “Z” direction, there is less resin where there is a strand of fiber and more resin in the areas between the “X & Y” fibers. The thicker areas shrink more than the thinner. This shrinkage transfers through to the face of the tool and shows the cloth pattern. It happens during the post-cure cycle and it only happens once, so if it is sanded and polished out, it does not return.
If no print-through is allowed, the only solution is to use very fine fabric for the first few plies and give the tool a slow heat-up rate to minimize shrinkage.
Mark-off is caused by the surface coat softening and allowing the production part to create a permanent mark on the surface. This commonly occurs during autoclave cycles where there is a combination of heat and pressure. The solution is to use a higher temperature rated surface coat and give it a proper post-cure before use.
What is the proper resin/fiber ratio for a laminate?
For every combination of resin/hardener and for each style of fabric, there is an optimum resin to fiber ratio. Tooling fabrics, because of their coarse open weaves, have higher resin ratios than production fabrics do. Laminates made by the contact lay-up method have higher ratios than laminates made by vacuum bagging.
The contact lay-up method of laminating, using tooling fabrics is primarily used for room-temperature service tools, i.e., holding, drilling and routing fixtures. These resin/fiber ratios are not critical, but should be kept around 50-55%. If resin is applied too liberally, excessive exotherm could cause problems. A contact laminate made by a skilled toolmaker who carefully wets-out the cloth should have a finished resin content between 45-50% resin.
It is recommended to start at 50% resin content when making vacuum-bag laminates for tooling. The excess resin is then pulled from the laminate by the bagging process. The ideal finished resin/fiber ratio for high-temperature tooling is 38-42% resin, depending upon the style of cloth being used.
Can a laminate be too wet?
Yes. High resin/fiber ratios can cause excessive exothermic heat buildup during the laminating process and be dimensionally unstable. Also high-temperature laminates with high resin ratios will develop excessive shrinkage during post-cure cycles. Most people will use too much resin because it makes it easy to wet-out the cloth. Getting the lower ratios means more time and effort working the resin out of the cloth.
Can a laminate be too dry?
Yes. Low resin/fiber ratios can cause delaminations between plies. Dry laminates create leak paths in tools requiring vacuum integrity.
Dry tools are caused by using improper laminating techniques such as not adequately wetting out the fabric with resin. Another cause of dryness is from excessive pressure being applied, if the tool is given an autoclave cure. Excessive pressure forces too much of the liquid resin out of the fabric.
What causes delaminations?
Low-resin content, improper compression, trapped air, improper surface preparation, and/or contamination result in delaminations between plies of a laminate.
Dry plies lack enough resin for the plies to get an adequate bond to each other. These plies will delaminate as the tool is worked or heat cycled.
Improper compression comes from either poor laminating technique or loss of vacuum-bag pressure before the resin gels. This results in the plies not being forced into contact with each other.
Air bubbles between plies of high-temperature tools expand and contract during heat cycles. These voids create starting points for delaminations.
If the resin in a laminate is allowed to cure hard before a subsequent ply is applied, the new ply will not properly bond. Before the new ply is laminated, the cured surface must be roughed up by sanding. A release ply or peel ply can be applied to the back of a laminate, if it is going to cure hard before the laminate can be continued. Once removed, the peel ply creates a good bonding surface for the remaining plies.
Airborne oil or mold release contaminates can settle on laminates while they are being made and cause a weak bond from one ply to another, which results in delamination.
What causes trapped air in a laminate?
Poor laminating technique is the primary reason for trapped air in a laminate. Other possible reasons are whipping too much air into the resin system while mixing, dry areas in the laminate, and bridging plies of fabric on inside corners. Vacuum bagging can minimize or eliminate these problems.
What is the recommended laminating procedure?
There are a number of acceptable methods of laminating. The procedure we recommend that has been proven to control resin/fiber ratios, control warpage and minimize trapped air is outlined here.
If resin content is critical, like for high-temperature close-tolerance tools, we recommend precutting the plies of fabric and weighing them. Then weigh out the total amount of laminating resin and hardener in batch sizes appropriate for the working time of the system. Make sure the total weight of the resin/hardener is the same as the cloth weight. During the laminating process, monitor the number of plies vs. the weight of laminating resin used. For example: If you have laminated 3 plies of a 12-ply laminate, only ¼ of the total laminating resin should have been used.
We recommend rotating the ply orientation, typically 0°, +45°, -45°, and 90°. This is especially important if the fabric is not a balanced weave. Also, never roll out full lengths of cloth on large laminates. Cut the lengths into smaller squares appropriate to the size of the tool. The first 3-4 layers should be butted together. Subsequent plies can have their edges overlapped, if desired.
Test have proven that less air is trapped while laminating if the resin is applied first and dry cloth applied to the wet resin. This procedure allows the resin to wick up into the cloth, pushing the air ahead of it. If resin is applied to dry fabric, the air has to pass through the resin to escape and tends to trap more air. Another method is to wet-out the cloth on a table (in effect pre-preging the cloth) and then place the wet plies on the work. This method is used for large jobs where one person is impregnating the cloth and others laminating. This method also forces air to pass through the resin and is easily trapped in the laminate.
On flat surfaces use a squeegee to apply resin. Squeegees and/or rollers can be used to compress and wet-out the cloth. For tools with contours and detail, a stiff brush (PTM&W Tooling Brushes) should be used to spread the resin and to compress and wet-out the fabric by stippling.
What causes a laminate to warp?
Laminate warpage is caused by unequal shrinkage where one area shrinks more than another, resulting in a build up of stress. This stress is relieved as the tool warps.
Laminates can warp when constructed with long lengths of cloth. It is best to use smaller lengths that can move easier when being compressed. Balanced ply orientation is important to minimize warpage.
A tool can also warp by using back-up structure that gives inadequate support.
If a tool is heated substantially above its Tg or HDT, it can warp. If heated too hot, the resin matrix can soften to the point where it does not have enough strength to support the shape of the tool.
What causes a laminate to shrink?
Compared to polyester or vinyl ester systems, epoxies have very low shrinkage. The amount of shrinkage is controlled by resin content, hardener speed, and the post-cure cycle.
All epoxy resin systems shrink to some degree. The higher the resin content of a laminate, the more shrinkage occurs.
There are two types of shrinkage, both caused by heat; primary and secondary. Primary shrinkage is caused by excessive exothermic heat from using a hardener that is too fast for either the mass of material being used or the ambient temperature of the shop. This shrinkage can be observed after a room temperature cure. Primary shrinkage can be controlled by the correct choice of hardeners for the conditions.
Secondary shrinkage is caused by heat from an external source applied during post-cure cycles and is observed after the final cure. Fast heat-up rates and short dwell times during step cures will cause more secondary shrinkage than if the same tool were step cured with slow heat-up rates and long dwell times.
Shrinkage is rarely equal in all parts of the tool. Unequal shrinkage directly leads to warpage
Why vacuum bag laminates?
Vacuum bagging is used to control resin content, remove trapped air and increase contact between plies of a laminate. At sea level, a laminate bagged under full vacuum will be compressed under 14.7 pounds per square inch. If proper bleeder and breather materials are used, vacuum bagging will remove excess resin from the laminate, along with any trapped air. This compression also forces each ply into intimate contact, for good interlaminar bonding.
Vacuum bagging is less effective when done at higher elevations because pressure decreases as altitude increases.
It is a common misconception that vacuum bagging can “bleed” a laminate too dry. Vacuum-bag pressure alone cannot stave a laminate. When additional pressure is added, such as during an autoclave cycle, it is possible to remove too much resin if excessive pressure is used.
What are the factors to consider when vacuum-bagging?
It is important to verify that the pattern used for making the tool is vacuum tight before laying up the laminate. A leak in the pattern or the bagging film will reduce the vacuum level inside the bag and cut the effective pressure being applied to the laminate. In addition, leaks can induce air into the laminate.
Vacuum bagging is only effective if done while the resin is still fluid enough to be moved out of the laminate into the bleeder material. As epoxies cure they become thicker and thicker until the point where they gel. At some point during this cycle, the resin becomes so thick it will not move under the pressure of the bag and the suction of the vacuum. This point is considered the working life of the material. If vacuum is applied after this time, it is useless.
The bag needs to be applied well within the working life of the resin that was laminated into the first plies of the laminate. A common mistake is to use a hardener with a working time that is too fast for the job. In this case, if vacuum is applied, it just pulls the excess resin and air from the last few plies of the laminate that is still liquid. This is material that has been freshly mixed and applied, and has no effect on the most critical first plies of the laminate.
Always allow plenty of time to get the job bagged because often times leaks occur in the bag and it takes time to resolve them.
One method to keep track of the working time is to make a small 6” X 6” laminate off to the side of the actual tool. For every ply of cloth applied to the tool apply one to the small laminate. As the laminate continues, check the first plies of the small laminate to make sure the resin is still fluid. When these plies indicate that the resin is thickening, it is time to get the tool under vacuum. Another way is to leave a small amount of resin from the first mix in a cup and watch it. If it starts to thicken, it is time to bag the tool.
If the entire thickness of the tool cannot be made within the working time of the resin, make only the number of plies consistent with that time. Apply vacuum until the resin gels. Then, remove the bag and start again on the remaining plies.
The first few plies of a high-temperature tool are the most critical for removing air. It is best to take extra care while laminating the first 2-4 plies and then bag these plies overnight. Subsequent plies are less critical, so more can be laminated before bagging.
Can wet lay-up tools be compressed in an autoclave?
Autoclave-cured wet lay-up tools can be made to the same quality levels as autoclave-cured prepreg tools. Care should be used because a liquid resin system will flow under pressure much easier than prepreg resins. It is easy to remove too much resin under autoclave pressures. Normally 30-40 psi is sufficient to tightly compress a wet lay-up laminate. It is important to install a trap between the laminate and the vacuum pump, as the liquid resin can be sucked into the pump.
The autoclave is used to pressurize the laminate until the resin gels. The tool can then be given a heat-set and post-cured in a conventional oven, thus minimizing expensive autoclave time.
As when vacuum-bagging, an autoclave-cured laminate must be under pressure within the working time of the resin system.
What causes the back of a laminate to be sometimes tacky?
If laminates are made with amine-based epoxy hardeners in high humidity conditions, the back surface of the laminate will sometimes be tacky to the touch. In some cases, it will be hard to sand and actually gum-up the sandpaper. This condition is known as “amine blush”. It is a natural reaction between the moisture in the air and the amine chemicals in the hardener.
Amine blush is strictly a surface phenomenon and is no indicator of how cured the laminate is. It also has no effect on the cured properties of the laminate. This tacky film can be washed off with soap and water or solvents.
Can laminating resins be thinned by using solvents?
Thinning epoxy resin systems with solvents is not recommended. Solvents can be trapped in the laminate as it cures, creating low mechanical properties and porosity. It is better to choose a lower-viscosity resin system to start with than try to thin an existing system.
How critical are times and temperatures of cure cycles?
Cure times and temperature cycles are suggested on the individual product data sheets. These are only guidelines. Tool thickness, contour, dimensional tolerance, resin systems and use temperature are factors which determine optimum times and temperatures. It is always safer to use slower heat-up rates, more dwell temperatures, and longer dwell times than to rush through cure cycles. The few hours saved by speeding through a cure cycle is often paid for by excessive shrinkage and warpage of the tool.
Published cure temperatures are recommended for the actual temperature of the tool. A common mistake is to just go by oven temperature. A thick cross section takes more time for the heat to soak through and reach the center than if is was thin. Once a tool has stabilized at a temperature, it should dwell there for enough time for crosslinking to occur.
If a tool is being cured on plastic-faced plaster, more time should be allowed for the heat to transfer from the back of the laminate all the way through to the face. The PFP takes a long time to heat, so the heat usually comes from the backside of the laminate.
Some resin systems are designed as “room-temp set, high-temp use”. Once a tool has cured at room temperature, it can be removed from the master and be given either a post-cure or placed in service. Hardeners for these types of systems are hybrids containing some components that cure at room temperature and others that cure at high temperature.
Even though the tool cures hard at room temperature, it will soften the first time it sees heat until the high-temperature portion of the hardener crosslinks. That is why we recommend a post cure before putting the tool into service. If placed in service without a post cure, like for example a vacuum-forming tool, it is best to give it a few production heat cycles without forming parts. This allows the resin to at least partially crosslink at higher temperatures.
If there are questions regarding a cure cycle, please call and ask for our technical service department.
How do you stop vacuum leaks in high-temperature tools?
If a tool has to be vacuum-tight for oven or autoclave use, it is best to make the tool with vacuum-bag or autoclave construction instead of contact lay-up methods. Properly done, these tools should not leak.
Never let production workers cut prepreg on composite tool surfaces.
If there are leaks in high-temperature tools they can be stopped by using the following method:
Lay a couple of plies of dry fiberglass cloth on the working surface of the tool, then bag the tool while placing a vacuum gage either on the tool surface or somewhere in the line between the tool and the vacuum pump shut-off valve. Pull vacuum on the bag, then close the valve and measure the vacuum drop on the gage. Mix PTM&W PT2050 with PH3210 hardener (100:30 pbw) and brush coat the entire surface of the tool that is outside the bag. Do this while the bag is under vacuum with the pump on. As this low-viscosity epoxy is applied, it will suck into any leak path, damming it up. As the leaks are plugged, the vacuum gage should start to climb. Allow the resin system to cure. To determine when all the leaks are filled, pull a vacuum on the bag, then turn off the pump and close the valve. The gage will not drop when the leaks are sealed.
What is an infusion resin system?
Infusion resin systems are specially formulated thermoset resins used in vacuum-assisted resin transfer molding (VARTM) or resin infusion processes. The resin is pulled through dry fiber reinforcement using vacuum pressure, allowing for high fiber volume parts with excellent surface finish and structural integrity.
What are the advantages of PTM&W infusion resins?
PTM&W infusion resins are designed for low viscosity, variable pot lifes, and excellent wet-out of reinforcements. Our systems offer:
- High strength and stiffness
- Low exotherm for thick section parts
- Controlled cure profiles
- Excellent clarity (where required)
- Compatibility with carbon, fiberglass, and aramid fabrics
Which PTM&W resin systems are best for infusion applications?
Commonly used PTM&W infusion systems include:
- MVS-610: Low Viscosity, room temperature infusion system. Ideal for any production applications, allowing quick turnaround for increased production.
- PT5760: High-temperature infusion resin suitable for aerospace-grade parts and tooling. Boasting a Tg of over 450𝇈F.
- PT5712: Low-viscosity epoxy system designed for vacuum infusion and high-temperature tooling. Provides void-free laminates with excellent strength and heat resistance.
Always consult technical data sheets for specific performance and cure profiles.
Can PTM&W infusion resins be used with carbon fiber?
Yes. PTM&W infusion epoxies are engineered for strong adhesion and effective wet-out with carbon fiber, ensuring optimal mechanical performance in structural composite applications.
What is the typical viscosity range of PTM&W infusion resins?
Most PTM&W infusion resins have a mixed viscosity between 200 and 1,000 cps at 77°F (25°C), making them suitable for full wet-out in tightly packed fiber layups and complex molds.
Are PTM&W infusion resins suitable for high-temperature applications?
Yes. PTM&W offers high-Tg infusion systems designed to withstand elevated service temperatures, especially after proper post-curing. Always verify Tg and thermal performance in the TDS.
Can PTM&W resins be colored or pigmented?
Yes. Most systems can be tinted using compatible epoxy pigments. However, color may affect optical clarity or final cure characteristics, so test samples are recommended before full production use. Always consult with a PTM&W representative with any questions about pigmenting.
Are PTM&W infusion resins compatible with vacuum bagging and release films?
Absolutely. These systems are designed for vacuum infusion and are compatible with common vacuum bagging materials, peel plies, flow media, and release films used in composite manufacturing.
How should PTM&W infusion resin systems be stored?
Store in tightly sealed containers in a cool, dry location away from direct sunlight. Nitrogen capping after each use will help extend shelf life. Avoid temperature fluctuations. Shelf life varies by product, but most systems offer 6 to 12 months of storage when kept under proper conditions.
How do you properly mix casting resins?
Proper mixing of casting resins is critical because soft spots or uncured material in the casting can result in tool failure or require rework. Improper mixing can increase the chance of trapped air in the casting.
When mixing casting resins, always “double-cup”. This simply means to weigh the resin and hardener in one container and thoroughly mix by scraping the sides and bottom of the container. Transfer the mixed material into a second container and remix in the same manner. This procedure eliminates the possibility of applying unmixed material.
Never mix in only one container, as there is a good chance that either the resin or hardener will cling to the sides, bottom or corners of the container and not be properly blended. Also, never scrape the sides of the container when pouring into the mold cavity.
What causes porosity in castings?
Aggressive mixing, improper pouring, moisture contamination and excessive exotherm can cause porosity in a casting.
When mixing casting resins and hardeners, avoid inducing air into the mixture by aggressive mixing action. Either stir the material with a spatula or use a mechanical mixer and drill motor. Some mixers, like those of the Jiffy Mixer line, induce less air than others. The best way to remove trapped air due to mixing is to vacuum degas (de-air) the mixture in a vacuum chamber before pouring.
Air can be trapped during the pouring process. If the casting is to be made as an open-faced pour, cast the material in a thin stream into the lowest part of the cavity. Allow the resin to flow out from that point as it pushes the air ahead of the flow. Do not pour the material back and forth causing it to fold over itself. If casting into a closed cavity, make sure the sprue (fill tube) is large enough so the resin can flow down without closing off the opening. Always have the sprue in the lowest part of the casting and provide adequate venting in the highest parts.
Moisture containing materials, like plaster and wood, should be properly sealed and released before castings are made against them. Otherwise, when the epoxy casting resin exotherms during the curing process, the heat will draw out the moisture and create surface porosity in the casting. Using sanding sealer, wax and PVC or PVA film barriers is the best way to protect the casting.
Choosing the proper hardener speed for the size of the casting and the ambient shop temperature will minimize exothermic reactions. If these reactions get hot enough, the casting resin will boil, creating porosity throughout the casting.
What is the proper way to deair a casting material?
Deairing (vacuum degassing) is used to remove mixed-in air from a casting material. Generally speaking, urethanes are easier to deair than epoxies. Epoxies have high surface tension, which makes it hard for air bubbles to break, even under vacuum. Adding a few drops of PA0550 Bubble Breaker helps to lower surface tension for easier deairing.
A leak-proof vacuum chamber and a good-quality vacuum pump are mandatory for deairing resin systems. Viewing ports in the vacuum chamber are quite helpful to determine when the degassing process is complete.
A common mistake made while vacuum degassing is to not completely remove the air from the resin. Incomplete air removal is due to inadequate equipment, vacuum leaks, or not letting the deairing process finish. Casting resin will expand from 3-5 times its normal volume while being degassed. Allow a large enough container to allow for this expansion to happen. Once the resin has expanded to its full height, the material will start to boil and soon collapse down to its original volume. At this point the vast majority of air has been removed. A few more minutes of deairing under full vacuum (if time allows) will remove most of the remaining air. If the material does not boil and fall (break) the air has only expanded and has not been removed.
Be aware that the vacuuming process generates heat in the resin mixture and will reduce the working time of the material being deaired.
What causes a casting to crack?
Cast molds crack due to built up stresses caused by excessive exotherm or improper cure cycles and thermal shock from fast heating and cooling during production cycles. Design problems such as internal sharp corners, thick-to-thin transitions and inadequate edge distances for holes or inserts can also cause cracking.
Cast tools are not as tough as laminated tools because they do not have the reinforcement that comes from cloth. Rough handling, like dropping the tool or prying them open, can cause cracking.
What causes soft castings?
If castings are soft in some areas and hard in others, it is due to improper mixing procedures. If the entire casting is soft, it is a result of either being mixed off ratio or not being fully cured. Always use the proper speed hardener for the size of the casting.
What causes excessive shrinkage?
There are two forms of shrinkage: primary shrinkage and secondary shrinkage. All thermoplastic resin systems shrink when they cure due to internally generated heat (exotherm) during the crosslinking process. This primary shrinkage can be observed after the casting has cooled and been demolded from the pattern. Selecting hardeners that are commensurate with the mass of material being cast and the ambient temperature of the shop can control primary shrinkage.
Secondary shrinkage is a result of applying external heat (oven) during post curing. This shrinkage can be observed after the final post cure. Using slow ramp-up rates, more dwell temperatures and longer time at each temperature can minimize secondary shrinkage.
What do shrinkage numbers mean on data sheets?
Published shrinkage numbers for casting resins are not meaningful unless the mold size used for testing is identified. ASTM D2566 test method uses different mold cavities for testing shrinkage. Each mold is a half round cavity, exactly 10.000 inches long. Total shrinkage is measured over the 10-inch length and reported in thousandths of inch shrinkage per inch of length. For example: In ASTM D2566 Mold #2 the shrinkage of a certain product is 0.003-inches/inch. (Over the 10 inches, the product shrinks 0.030 inches.) The same product in a #3 mold may shrink 0.010-inches/inch.
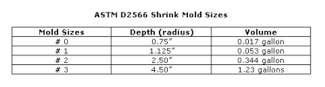
Published shrinkage numbers are only to be used for comparing one product to another that has been tested in the same size shrink mold. These numbers are not to be used in predicting actual shrinkage of a cast part or tool.
How can shrinkage be minimized for large castings?
Casting shrinkage can be minimized by choosing a hardener with the correct speed for the job, pouring less mass per cast (use multiple pours if necessary), adding bulk filler, controlling the ambient temperature during casting, and using slower post-cure cycles.
What types of bulk fillers can be used to control shrinkage?
The only constraint regarding using bulk fillers for epoxies to control shrinkage is that they should not contain moisture. If weight and machinability are not issues, dry sand, limestone, and pea gravel are cheap and effective fillers. If weight is an issue but not machinability, microballoons, volcanic rock, and walnut shells can be considered. For castings that need to be machined, use aluminum powder. If heat transfer is the main concern, use aluminum powder or particles.
How can thermal conductivity be increased?
Adding high-conductivity fillers can increase thermal conductivity of a casting resin. Aluminum shot, granules or needles are the most cost-efficient types of bulk fillers to use for increasing heat transfer. With some of our aluminum-filled (powder) casting resins, more than two times the weight of the resin/hardener can be added as aluminum filler.
To get the maximum amount of bulk aluminum filler into a casting resin, mix the resin and hardener together than add an equal amount of filler. This should make a concrete-slurry consistency. Once this blend has been cast into the mold, add dry aluminum filler to the back of the casting. If the casting is on a vibrating table, the filler will quickly sink to the bottom and more filler can be added. Keep adding filler until the casting is packed solid with aluminum.
No matter how much filler is added, conductivity of the casting resin will never be that of solid aluminum. Even a casting with the highest concentration of aluminum has each particle of aluminum coated with epoxy, which is an insulator.
Can casting resins be thinned by solvents?
Never thin epoxy and urethane casting resins by adding solvents to the mixture. Solvents that have not evaporated before the resin system gels will remain in the cast material and weaken its structure.
How can casting resins be thinned?
If a casting resin system is too thick for the application, choose a thinner resin/hardener combination or warm the system to lower its viscosity. Be aware that warming will shorten gel times and increase the level of exotherm.
What is a urethane?
Urethanes are named for the urethane group that is formed when an isocyanate component (urethane resin) and the hydroxyl or amine component (urethane hardener) react. This kind of plastic is known as a thermoset, because the urethane reaction is not reversible with heat or pressure, these thermoset urethanes do not melt or flow. Epoxies are also thermosets, but are named for the reactive epoxy group that you start with before cure. There are no epoxy groups left in cured epoxies.
What can cause urethanes to bubble?
Like many other 2 part systems, urethanes can trap the air stirred in during the mixing of the resin and hardener. This trapped air is easily removed by pulling a short vacuum on the mix before pouring the part. Additionally, bubbling in urethanes is caused when the isocyanate component (urethane resin) reacts with water. This isocyanate/water reaction generates carbon dioxide gas or bubbles. Water pick up can come from moist air, or even paper, or wood mixing equipment. The urethane resins and hardeners as supplied have extremely low moisture content, and will not bubble when mixed, so that very nice bubble free castings can be made with just a vacuum step after mix, if plastic or metal mixing equipment is used.
Are urethanes sensitive to mix ratio?
Two part urethanes, like two part epoxies, need the correct quantity of resin and hardener groups for best results. Unlike epoxies, there are no “variable mixing ratio” urethanes. Mixes using excess urethane hardener may cure to a solid, but the excess hardener groups will attract moisture into the cured part, and always give inferior physical properties. Larger excesses of hardener may give cures that are sticky, or semi-solid “goo’s”. Mixes with large excesses of isocyanate (urethane resin) may remain liquid after cure, or mixes with small excesses of isocyanate may form low melting thermoplastic waxes, or brittle solids. Carefully weighing the correct amounts of both urethane resin and urethane hardener will ensure best results.
How should I store my urethane between uses?
As the isocyanate (urethane resin) reacts with water and can skin over like a can of paint, or build up carbon dioxide pressure if stored with wet air in the head space of the container it is best to carefully purge, or displace the wet air with dry nitrogen, and then carefully seal the container between uses. The urethane hardener can also pick up moisture from wet air in the head space, and while no skin forms, or pressure build up occurs, in extreme cases enough water can build up, so that bubbling can occur when mixed with the urethane resin. For best storage put the dry nitrogen cap on both the resin and hardener between uses. Extremes of heat or cold for storage should be avoided, with the storage sweet spot being at 60°F to 90°F, and the use temperature sweet spot being 70°F to 80°F. Today’s urethanes, as formulated, will withstand a fair amount of abuse during storage or processing, but the very best results are achieved with a little extra care with the dry nitrogen cap, and with the use, and storage temperatures.
How can I color my urethanes?
Urethanes can be colored by adding a few percent of a paste color dispersion either to the mix just before the vacuum step, or by adding to the polyol (hardener side) before the mix if more time is needed to tint to the correct shade. Both the color dispersions made for urethanes, and those made for epoxies work well. Even the tubes of “Artists Oil Paints”, or universal color dispersions for oil based paint work well. Do not use universal color dispersions designed for water based paint, as these have water or alcohol’s that cause the urethanes to bubble. Do not use solvent containing color dispersions, as again this will cause bubbling and loss of properties. Do not use more color than you need to get the color depth you desire, because larger amounts generally cause some loss in properties. Be sure to maintain the correct Resin to Hardener ratio. For example, if the correct mix ratio is 100 parts by weight of urethane resin to 50 parts by weight of urethane hardener, and you are going to add 2 parts by weight of color dispersion to the urethane hardener, then the final mix ratio becomes 100 parts by weight of urethane resin to 52 parts by weight of the urethane hardener/color dispersion blend.
What should I do for urethane cleanup?
Urethanes should be cleaned promptly off equipment before cured, as cured residues are tough to remove. Promptly wipe, drain, or spin off the excess liquid, uncured urethane, and then use a small amount of solvent to remove any residues. Flammable solvents, like Acetone, require care to avoid static or any spark (such as an electric drill) in the area, as flammable fumes can accumulate giving rise to fire or explosion hazards. Non flammable solvents, like Methylene chloride, also require care as accumulated fumes can give rise to health hazards. Wherever possible, use disposable plastic coated paper mixing cups or tubs, to minimize cleanup problems.
How much heat or cold will cured urethanes take?
Soft urethanes will withstand extreme cold, and can remain flexible to far below sub zero. Hard urethanes can be formulated that will maintain their hardness, and other mechanical properties at upwards of 250°F.
What kind of physical properties should I expect from a cured urethane?
Urethanes can be formulated to cover a wide range of hardness, everything from very soft rubbers to hard plastics. In general, urethanes are known to excel at having better abrasion resistance at every hardness than a comparable rubber or plastic made from another kind of polymer. Urethanes can also exhibit very good low temperature properties, staying flexible when many other polymers become brittle. In addition, urethanes have an overall balance of high elongation, tensile strength, flexural strength, and tear strength that yields tough, durable products that can be processed by liquid casting without expensive tooling.
How Critical is the Mix Ratio?
The answer is; it depends on the system. Epoxies are not like polyester resins where basically any amount of hardener will allow the laminate to cure. Epoxy resins and hardeners have calculated “fixed” ratios, which allow their individual molecule groups to cross-link completely with one another. Careful measurement of the two ensures that ultimate properties for a given system are achieved on a repeatable basis.
A high performance laminating resin and hardener such as PR2032 and PH3660 with a mix ratio of 100:27 parts by weight (pbw), require that level of accuracy to obtain the physical properties we state on our technical data sheet. Generally we like to see that within a range of 100:25-100:29 pbw. Our lab worked hard to arrive at a volumetric mix ratio of 3:1 for builders without scales to help eliminate “guesswork.”
It is important to note that the target mix ratio should be the one that is published. The tolerance range allows for slight errors in measurement. To intentionally measure off ratio is never advised. Some epoxy hardeners are formulated to be “variable-ratio hardeners”. The published ratios for these hardeners will show a range of acceptable mix ratios.
Exceptions to this rule are the Aeropoxy adhesives and Lightweight filler. These are 1:1 and 2:1 respectively by weight or volume. 1:1 and 2:1 systems have inherent “fudge factors” built in due to the higher mix ratios. Obviously anytime you are bonding critical structural components it’s advised to be as accurate as possible. As a rule of thumb remember the lower the mix ratio (100:10 for example) the higher the required degree of accuracy.
Is Aeropoxy Compatible With Other Cured Epoxies?
Yes. Epoxies are inherently good adhesives. They will bond together quite well if the surface is prepared properly, i.e. a clean, scuffed or sanded surface.
The exception to this would be some sort of specialty epoxy, such as one that had unusual additives or fillers to enhance particular properties, chemical resistance and/or finish. If that is the case, you would need to consult with the manufacturer of the specialty system for their recommendation.
How Well Does it Bond to Metal? Wood? Styrofoam?
The AEROPOXY product line was developed with all of these materials in mind. Choosing the proper system for the job at hand being the main consideration. As in any bonding application, surface preparation is the most important aspect of the process. If you are unsure of the proper AEROPOXY system for your bonding project, consult with a PTM&W representative.
Why is the Back of the Laminate Tacky the Next Day?
There are several reasons why this can occur. First, the mix ratio could be off. Under or over catalyzed epoxy resins can have the same net effect – rubbery and/or tacky laminate. Second, if the temperature is below 65°F, chances are the laminate has not fully cured, leaving a tacky finish. Third, in extremely humid conditions, moisture can react with the uncured surface forming a tacky compound, called carbamate. This carbamate will not affect the cured properties of the laminate, but will affect adhesion of subsequent layers of epoxy if not removed prior to laminating. The easiest way to prevent this potential problem is to peel ply the final layer of your laminate, protecting the epoxy from the moisture.
It should be noted; laminating in high humidity conditions will not affect the cured properties of the laminate. The tacky condition described above will only occur while the laminate is gelling or curing.
Can AEROPOXY be Used for Major Structural Areas?
Yes! The AEROPOXY PR2032 / PH3660 laminating system was developed for tough, high performance structural applications. You can expect high physical properties along with excellent heat resistance in your well-designed, properly laminated parts or tooling. For areas where a structural bond is required, we would recommend either ES6228 or ES6279 paste adhesives in conjunction with the laminating resin.
Will AEROPOXY Bond to Carbon Graphite and Kevlar Fabrics?
Yes! The PR2032 / PH3660 laminating system has been used extensively in the fabrication of high performance carbon graphite and Kevlar parts. Test results show excellent physically properties can be achieved when using these fabrics. Refer to the technical data sheet for physical properties.
Can PR2032 / PH3660 be Used with Fillers?
The answer is yes. The AEROPOXY system works very well with the addition of microballons, cotton floc, milled fibers, and many other fillers adding excellent diversification. Having said that, PTM&W developed the AEROPOXY line of resins with specific uses in mind, i.e., laminating resins for composite laminates, pourable and paste adhesives for structural bonding and a lightweight filler for finish sanding, lightweight fillets and build-up of non-structural areas.
Can PR2032 / PH3660 be Thinned to Reduce its Viscosity?
No. This is a high performance laminating resin system designed for specific uses. The viscosity, handling and cured properties are balanced and optimized to provide the best results possible. The resin and hardener were developed as a “tuned system” and should not be altered in any way. Special additives were incorporated to enhance the “wet-out” of all fabrics readily. The addition of solvents will not only change the viscosity but could alter the pot life, physical properties, Tg, and bring into play a host of other problems both known and unknown.
The vast majority of people complaining about the viscosities of epoxies are normally former polyester users. Polyesters are generally in the 300-500cps ranges. The main problem with materials too low in viscosity is the tendency for them to run or slump. The accumulation of resin in the low areas can result in unbalanced, resin-rich laminates. This fact is accentuated even more-so with the longer pot life resin systems, since they stay liquid longer.
Will the Resin or Hardener Freeze?
Epoxy resins and hardeners do not “freeze” to a solid at a certain low temperature, as does water. Some epoxy hardeners can crystallize at low temperatures, and some epoxy resins will do the same, to a lesser extent. The consistency of these products can range from hazy liquid to a loose, slushy semi-solid, even, in some extreme cases to a waxy solid. This is a general statement about epoxies, and does not refer to the Aeropoxy materials. The AEROPOXY product line was formulated not to crystallize in normal shipping and storage conditions, and we have not been able to cause any of the Aeropoxy product line to crystallize in the lab. Since there is rarely such a thing as an absolute certainty, we want to make you aware of what crystallization entails and what can be done if in fact it occurs.
First, it should be noted that a crystallized material is not ruined, or even changed. The condition is easily reversed. If a resin or hardener has crystallized, it can be returned to normal by heating it slightly. Warm the material over low heat. A hot plate on low works well, as well as a warm water bath that you’d set the can into. A temperature of 100°F-120°F is sufficient to dissolve the crystals. The material can then be used after it has cooled to room temperature.
It is fact, once a material has crystallized it is impossible to redissolve every single tiny crystal and some will remain in the material, although you may not see them. These will not impede the reaction when mixed, or change the cured properties. If however, all the material is not used, these seed crystals will reinitiate the solidification process again rather rapidly. Therefore any remaining material that is stored should be checked closely before being used again, if it looks hazy the safe bet would be to warm it again.
Does AEROPOXY Burn?
None of the AEROPOXY products are flammable materials, so there are no fire hazards associated with them, as there would be with solvents, for example. Being organic materials, they will support combustion, but they will never be the ignition source.
Epoxy materials can be made in fire retardant or self-extinguishing versions. These materials are designed to stop burning very soon after the fire source is removed. They are not non-burning materials. With the AEROPOXY line, we have developed products that have very high performance and high heat resistance. The use of fire retardant additives would diminish the performance and lower the heat resistance of the AEROPOXY product line. Should future regulations or market conditions require fire retardant products, we can provide them.
What Finish is Recommended for the Fiberglass Reinforcing Fabric?
When glass fabrics are manufactured, the individual warp and fill strands are coated with various binders and sizings to improve handling during construction. Since these binders can detract from the adhesion of the resin system and lower performance of the structure, it is best to use fabric that has had the sizing removed. Fabric manufacturers typically remove binders and sizing by heat or scouring, and glass fabric thus cleaned is called greige goods. Glass fabric is sold as greige goods, or with a coupling agent applied. Coupling agents, or finishes, are chosen based on compatibility with the polymeric resins. Finished fabrics generally provide improved wet-out and higher performance in the part or structure. The original finish for glass fabrics was Volan, developed by Dupont. Volan is still popular because it gives good performance with both epoxy and polyester resins. More recent technology finishes include various silane coupling agents designed for specific resins, which give higher physical properties because they are “tuned” to that specific resin.
Often, individual fabric weavers have their own number for the different finishes, so it is impossible to list all of them here. The important thing to remember when ordering fabric for your AEROPOXY project is to specify either a Volan finish or a silane that is designed for the best performance with epoxy resins.
When Preparing Surfaces for Bonding, Should You Solvent Clean, or is Air Blow-off Sufficient?
In cleaning metal surfaces for subsequent bonding, it is best to first solvent clean the metal, then abrade the surface to be bonded, followed by a final solvent clean to remove loose particles generated by the abrasion. Additionally, there are safe metal etching products (phosphoric acid) available at local hardware or home improvement stores that not only etch but clean the surface as well. The Aladine or uredine metal treatment systems available are designed to protect and prevent corrosion of the metal but may not be practical to use for the home-builder. You should consult with the applicable supplier if you are considering using these products.
In cases of metal bonding when solvents are used to clean the surface, always make sure you use new, clean solvent to prevent contamination and bond failure. Avoid reclaimed solvents, as their exact makeup cannot be determined and the possibility of contamination or adverse reactions are too high.
For composites surfaces, an initial solvent wipe of the surface to remove any grease or oils is acceptable. After the solvent dries, the area to be bonded should be sanded to roughen it up and increase the surface area. Then, the sanded surface should be blown off with compressed air to remove loose particles and dust from sanding. Since there is a possibility that a solvent might wick into the composite through the sanded area, solvent wiping after sanding is not recommended. While the use of a 40 grit sandpaper will increase the overall surface area you are bonding to, such a rough paper can damage the fibers in a given cloth matrix and potentially weaken your laminate. The question is whether you’re sanding to add additional layers of reinforcement or preparing for a finishing system. Note: See “Why Use Peel Ply” for additional option.
Why Use a Peel Ply? Does a Peel Ply Starve a Laminate?
The use of a peel ply, or tear ply, offers several benefits when constructing a laminate with epoxy resins. It’s a fabric that is applied over the last layer of cloth before the laminate is allowed to begin its cure. Since it does not bond to the laminate, it will peel off when and if, additional laminating or bonding is ready to continue. It’s often used when the lamination process has to be halted before all the plies of cloth have been applied. It leaves a roughened surface that does not require further preparation before laminating or bonding continues, i.e. sanding/scuffing the laminate.
The reasons to use a peel ply far out-way any objections not to. First, as mentioned, there is virtually no preparation necessary before continuing laminating or bonding (with the exception of areas where the peel ply wrinkles and you’ll have resin rich ridges that are easily sanded or ground off). Second and very important, peel ply protects your laminated parts from dirt, dust and contaminates that they may be exposed to over many days, months or even years before they’re needed. Third and maybe the most beneficial, it leaves a much smoother finish on the laminate than you would otherwise have. It minimizes pinholes and virtually eliminates the weave of the cloth, which eventually has to be filled in during the “finishing” process.
A number of types of peel ply materials are commercially available. These include, Teflon coated fiberglass fabric, fiberglass fabric coated with other release agents, as well as coated and uncoated nylon fabrics. Some AEROPOXY users have had good results with very tight weave Dacron fabric purchased from sewing centers and retail fabric shops.
It is highly unlikely that the use of peel ply will starve a laminate. The technique of applying a peel ply involves laying it on the back of a wet laminate and pressing it into intimate contact. The goal is to lay it on as smooth and wrinkle free as possible, while avoiding trapping air pockets under it. Peel ply fabrics are tightly woven, which minimizes the penetration and collection of resin, so the amount of resin removed with the peel ply is minimal when it is torn away. The tendency for amateur builders is to use more resin than necessary, resulting in a resin-rich laminate. The use of peel ply will help to control this common fault.
Do I Have to Post Cure My AEROPOXY Laminate? Does Post Curing Improve the Performance?
The Aeropoxy laminating systems will cure completely at normal room temperature and do not need a post cure to achieve the full properties listed on the literature. However, we always suggest that if you can, post cure the part.
A beneficial aspect of post curing is that the laminate gets to full cure much faster than if allowed to room temperature cure alone. This is especially important if you are on a tight schedule and want to move a laminate around, or remove it from a fixture to make another part. If this were done too soon, with only a partial, insufficient room temperature cure, there could be distortion of the laminate. On the other hand, if the laminate is post cured after a short room temperature cure, it has full properties and can be moved, worked on or assembled without worry of damage or distortion.

Ready To Get A Quote And Learn More?
Explore our wide range of products and services, and see how we can be the perfect fit for your needs. If you have any questions or need assistance, don’t hesitate to reach out! When you call, you’ll always speak with a real person—no automated menus, just expert support ready to help. Our team has the technical know-how to ensure you get the most out of our products. Let’s make things work for you!
If you’re looking for advanced solutions in Prepregs, Adhesive Films, Adhesive Pastes, and Equivalent Products, please refer to our partner company, MAKO Advanced Materials.